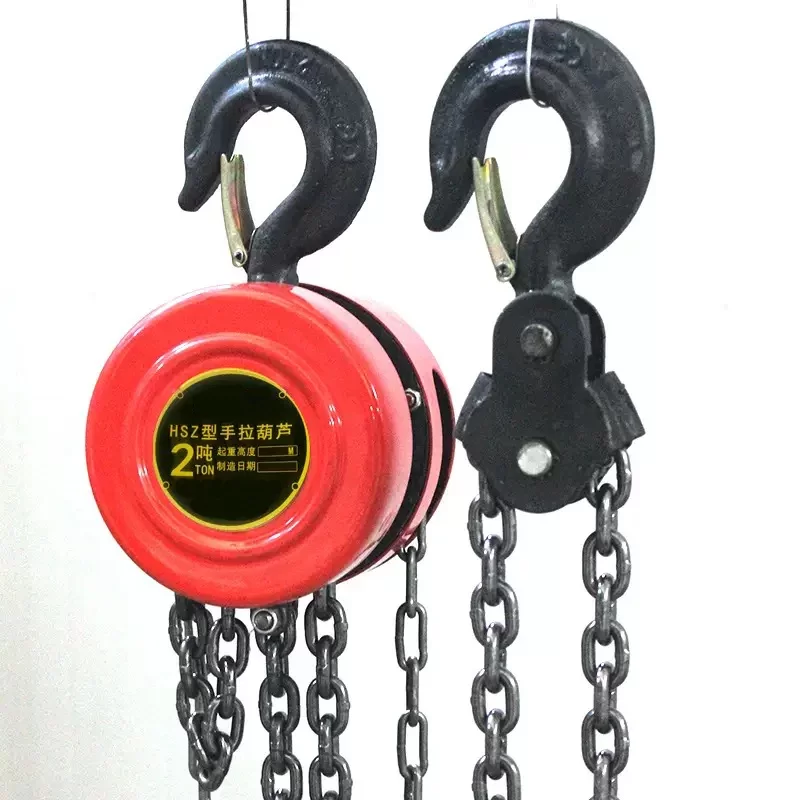
Industrial facility managers and procurement specialists frequently face a critical dilemma: balancing operational safety with load versatility. Utilizing unverified lifting equipment exposes your site to severe safety hazards, unexpected downtime, and non-compliance penalties. When operations require shifting capacities—from delicate machinery adjustments to moving heavy raw materials—securing a reliable ce certification chain block 250kg or 5 tons becomes the cornerstone of a secure operational workflow.
We understand that equipment failure is not an option. That is why our manufacturing ecosystem is designed specifically to solve these rigorous industrial demands. Operating from a state-of-the-art 13,000-square-meter facility in Baoding, China, our operations have been independently audited and verified by TÜV Rheinland. Established in 2005, we bring over a decade of dedicated research and development directly to your site.
By implementing a completely scientific quality management system, we eliminate the guesswork from procurement. Whether your facility needs the precision of a 250kg hoist or the brute strength of a 5-ton block, our CE and RoHS certified equipment guarantees immediate compliance for critical markets across North America, Western Europe, and beyond. This commitment to engineered safety ensures your workforce remains protected while your operational efficiency scales effortlessly.
Evaluating industrial lifting mechanisms requires a deep dive into the underlying engineering, material science, and manufacturing protocols. The structural integrity and functional reliability of your lifting blocks must align with strict international parameters. Below, we detail the core technical benchmarks that make our ce certification chain block 250kg or 5 tons the standard for high-stakes environments.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Regulatory Compliance | Guarantees equipment meets stringent health, safety, and environmental protection benchmarks. | CE and RoHS Certified; Trade capacity verified by TÜV Rheinland. | Frictionless integration into heavily regulated markets like Western Europe and Oceania. |
| Load Versatility | Allows single-vendor procurement for varied weight classes across diverse operational zones. | Precision calibrated across the spectrum, from light duty (250kg) to heavy duty (5 tons). | Reduces procurement complexity while ensuring uniform safety protocols across all capacities. |
| Quality Assurance | Minimizes the risk of catastrophic load failure and mechanical breakdown under stress. | Scientific quality management system perfected over 10+ years of R&D. | Delivers consistent, repeatable, and flawless operational safety for heavy rigging. |
| Production Scale | Ensures rapid fulfillment and consistent material availability for large-scale orders. | 13,000 sqm plant area; Supported by 10 strategic supply chain partners. | Guaranteed uninterrupted supply via Tianjin Port to South America, Middle East, and global hubs. |
Long-term financial performance in industrial sectors relies heavily on the durability and lifecycle of the infrastructure investments you make today. Procuring a premium ce certification chain block 250kg or 5 tons transcends standard capital expenditure—it is a strategic move in value engineering. By drastically reducing mechanical failure rates, mitigating compliance fines, and accelerating workflow speed, your operations directly capture a higher return on investment (ROI).
Market authority provides the ultimate proof of value. With an annual global revenue between US$5 Million and US$10 Million, our lifting solutions have earned an exceptional repeat buyer choice rate ranging from 50% to 80%. This metric explicitly demonstrates that global partners in regions like Southeast Asia, Africa, and the Domestic Market consistently experience the financial benefits of reduced downtime and extended equipment lifespans.
Related products
Top Selling Products


For industrial enterprises and logistics providers, securing reliable lifting equipment is paramount for operational safety. The wholesale hst type chain block represents a specialized category of manual lifting tools designed for high-load capacities and precise vertical movement. This article provides a technical deep dive into the selection, procurement, and application of these essential devices in professional environments. Navigating the B2B market for lifting gear requires more than just comparing prices; it involves an analysis of load-bearing certifications, material grades, and the operational environment of the facility. Whether used in construction sites or manufacturing workshops, the efficiency of a chain hoist directly impacts productivity

For industrial projects and construction sites, the ability to move heavy materials vertically with absolute precision is not just about efficiencyit is a critical safety requirement. The 220V Electric Wire Rope Hoist is specifically engineered to bridge the gap between compact design and heavy-duty performance. Whether operating in hazardous petrochemical zones or on complex bridge construction sites, professionals require lifting tools that balance operational stability with a low cost of ownership. By integrating advanced motor testing and international safety certifications, this equipment ensures that materials are transported securely without compromising productivity.