Procuring industrial lifting equipment often presents facility managers and procurement officers with a critical dilemma: balancing cost-efficiency with uncompromising worker safety. In demanding environments where material handling operates at maximum capacity, unexpected downtime or equipment failure is not just an inconvenience—it is a severe operational hazard. Navigating the global market to find a verified source that consistently delivers durability without inflating your budget can feel overwhelming.
The solution lies in identifying an industry-leading facility that merges rigorous scientific quality management with decades of specialized production experience. Since 2005, we have continuously optimized our 13,000-square-meter plant in Baoding, Hebei, to eliminate these supply chain risks. By integrating comprehensive TÜV Rheinland verification and stringent CE/RoHS compliance protocols, we transform supply chain uncertainty into absolute operational confidence.
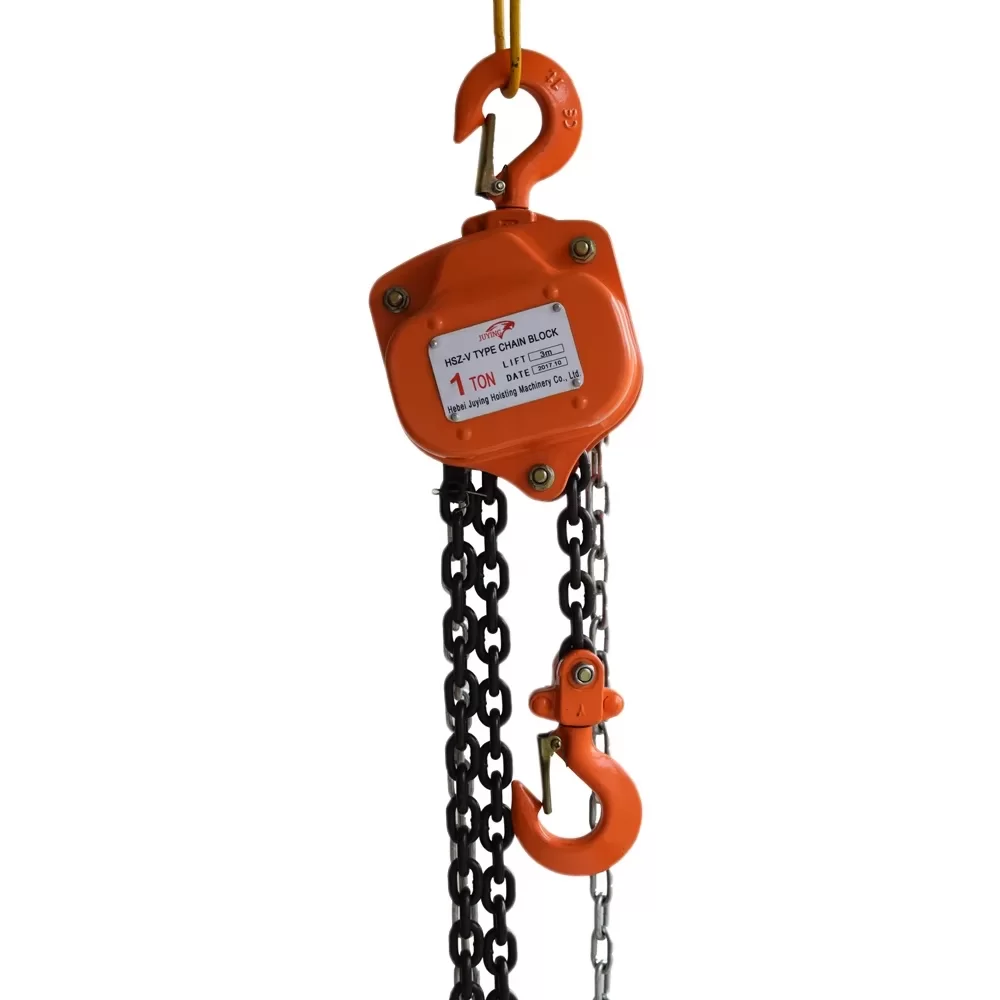
Selecting us as your dedicated ce certification heavy duty or hsz chain blocks manufacturer means securing a partnership rooted in transparency and performance. Backed by a robust team of 91-200 specialized personnel and over 10 active supply chain partnerships, we ensure every multifunctional hoist, manual stacker, and chain block delivered to ports like Tianjin meets elite global standards.
Technical superiority in the hoisting machinery sector requires more than just assembling components; it demands a systematic approach to research, development, and stringent quality control. To remain competitive across North America, Western Europe, the Middle East, and beyond, a credible supplier must adhere to measurable engineering benchmarks that guarantee longevity and safety.
Below is a detailed technical breakdown of the performance parameters that distinguish a world-class ce certification heavy duty or hsz chain blocks manufacturer from standard industry alternatives.
| Performance Metric | Industry Significance | Our Engineering Standard | Advantage |
|---|---|---|---|
| Safety & Compliance | Ensures operator protection and legal operational status in highly regulated zones. | Strictly maintained CE and RoHS product certifications. | Zero compliance friction for imports; guaranteed safe deployment in harsh environments. |
| Quality Management | Determines the consistency and defect rate of large-scale wholesale orders. | Scientific quality management system verified by TÜV Rheinland. | Yields an exceptionally high repeat buyer choice rate of 50% to 80%. |
| Production Capacity | Dictates lead times and the ability to fulfill bulk industrial requirements quickly. | 13,000 square meter audited plant with over 10 years of R&D experience. | Agile scaling for global demand, supporting an annual revenue of US$5M - $10M. |
| Product Diversification | Allows clients to consolidate supply chains under one trusted vendor. | Full spectrum: chain hoists, electric winches, wire rope hoists, and hydraulic stackers. | Streamlined logistics from Tianjin Port, lowering overall shipping and administrative costs. |
Strategic procurement is inherently linked to long-term financial performance. Investing in unverified lifting technology frequently leads to hidden costs, including accelerated wear-and-tear, frequent maintenance intervals, and compromised project timelines. Conversely, aligning your operations with an audited, high-tier supplier drastically reduces Total Cost of Ownership (TCO).
By leveraging an established ce certification heavy duty or hsz chain blocks manufacturer, organizations tap into immediate value engineering. Our impressive 50% to 80% repeat buyer rate is a direct reflection of this financial advantage. Clients spanning South America, Southeast Asia, Oceania, and Africa return because our heavy-duty solutions consistently outlast industry averages, safeguarding their bottom line.
Related products
Top Selling Products


For industrial enterprises and logistics providers, securing reliable lifting equipment is paramount for operational safety. The wholesale hst type chain block represents a specialized category of manual lifting tools designed for high-load capacities and precise vertical movement. This article provides a technical deep dive into the selection, procurement, and application of these essential devices in professional environments. Navigating the B2B market for lifting gear requires more than just comparing prices; it involves an analysis of load-bearing certifications, material grades, and the operational environment of the facility. Whether used in construction sites or manufacturing workshops, the efficiency of a chain hoist directly impacts productivity

For industrial projects and construction sites, the ability to move heavy materials vertically with absolute precision is not just about efficiencyit is a critical safety requirement. The 220V Electric Wire Rope Hoist is specifically engineered to bridge the gap between compact design and heavy-duty performance. Whether operating in hazardous petrochemical zones or on complex bridge construction sites, professionals require lifting tools that balance operational stability with a low cost of ownership. By integrating advanced motor testing and international safety certifications, this equipment ensures that materials are transported securely without compromising productivity.